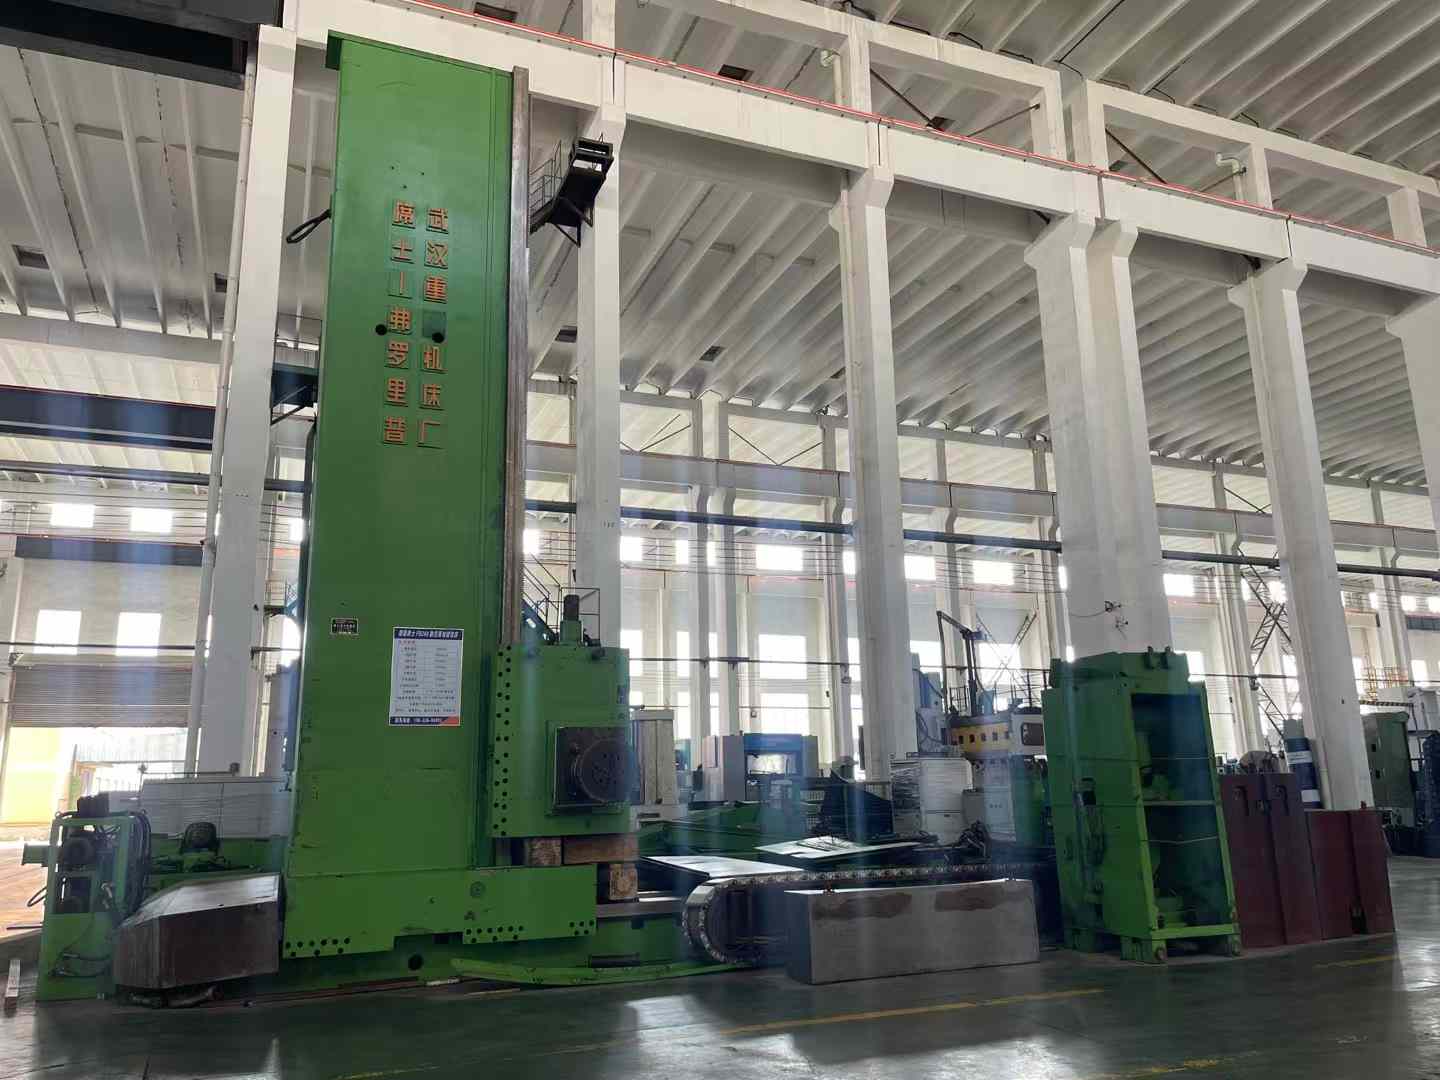
How to Select a Boring Machine for Heavy Equipment Repair and Maintenance
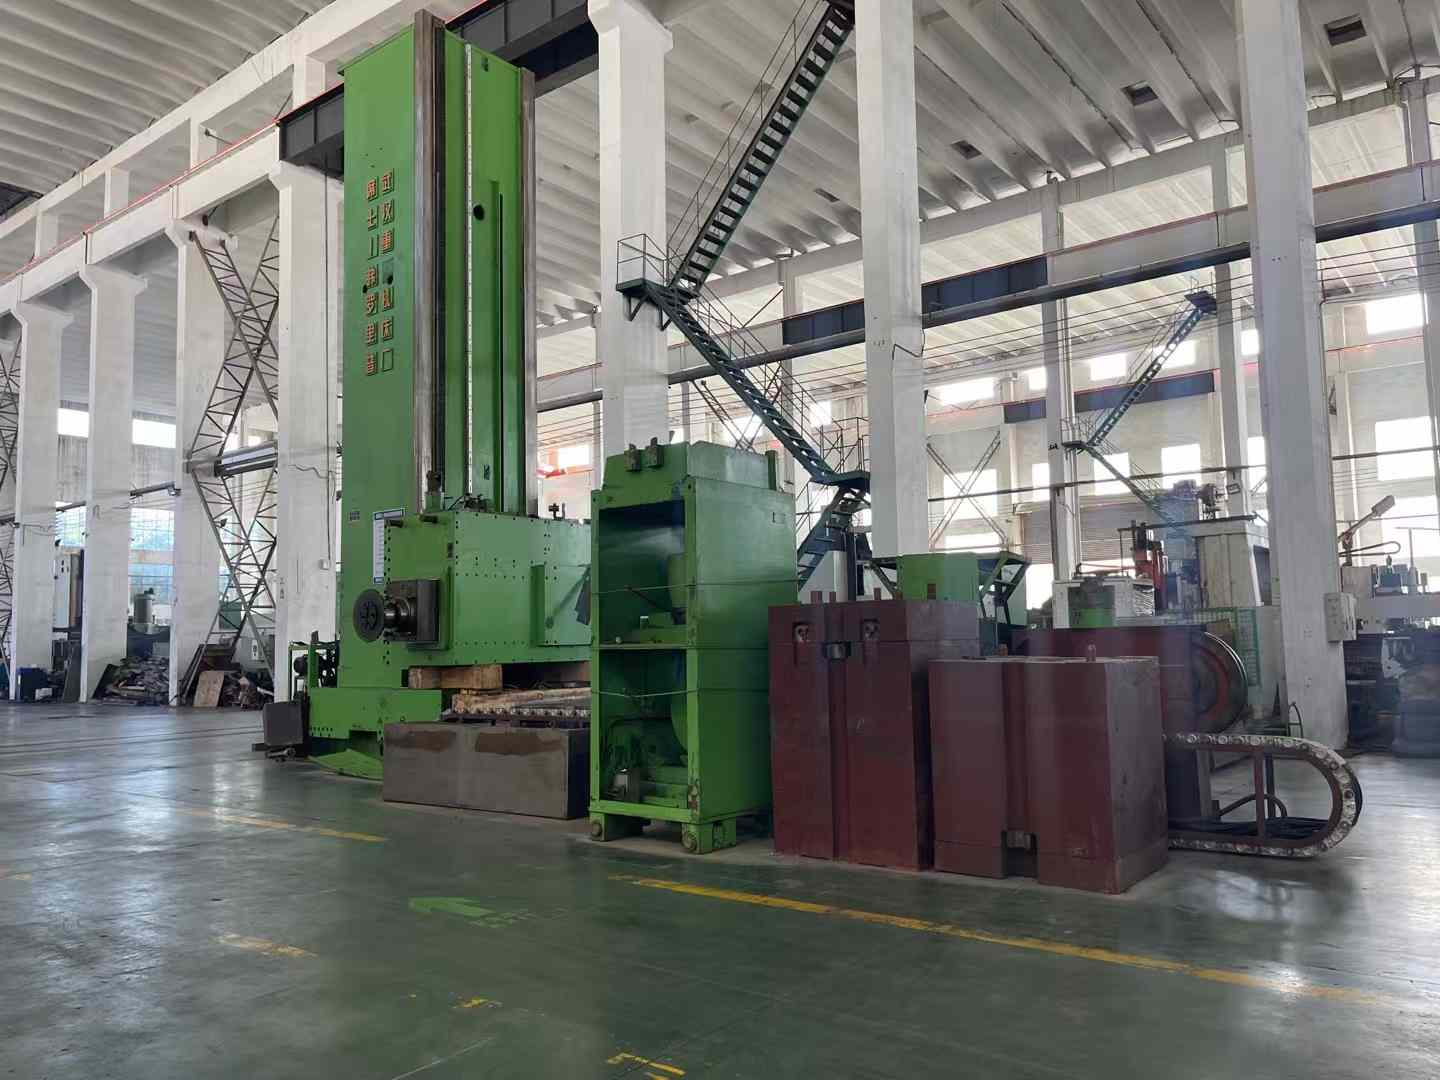
When an excavator, loader or crane develops play at a pin joint, the repair decision starts with the damaged bore and where the work must be done. Selecting a boring machine for heavy equipment means matching the machine’s working range and setup to the equipment, bore geometry and repair environment, not choosing by machine size alone.
Start with the equipment and bore
Repeated loading, vibration and movement can wear pivot bores out of round or enlarge them. Damage may affect a boom, arm, bucket, blade, steering joint, stabilizer or other connected structure. Bulldozers and mining machinery can present similar issues, often with limited access and substantial components that are difficult to transport.
Before comparing machines, identify the bore location, nominal and measured diameter, bore length, spacing between bores, and whether the holes must share a common axis. Also note obstructions, available mounting points and the clearance needed for the bar, supports and drive. These details define the required working range and setup options for heavy equipment line boring.
Match the machine to the repair setting
| Repair scenario | Selection priority |
|---|---|
| Excavator boom, arm or bucket joint | Bar reach, mounting access and alignment across separated bores |
| Loader linkage or articulation joint | Setup flexibility around the frame and room for the drive and supports |
| Bulldozer blade or ripper attachment | Access around large structures and practical positioning at the machine |
| Crane pivot or stabilizer connection | Clearance, stable mounting and the required bore length |
| Mining machinery with limited shutdown access | Transportability, on-site setup requirements and available power |
For on-site boring repair, consider whether the machine and accessories can be moved to the equipment, whether the work area allows safe setup, and what power and lifting support are available. If the component can be removed and handled in a workshop, compare that option with field machining based on transport, downtime and access constraints.
Check configuration before purchase
Compare the machine’s stated bore-diameter range, bar length, support arrangement, drive configuration and mounting method with the actual jobs you expect to handle. Confirm whether the configuration can accommodate the bore spacing and access limits, and whether the required accessories are included or optional. A nominal diameter range alone does not confirm that a machine can reach a particular joint or maintain the required alignment.
Share equipment type, bore dimensions, distance between bores, photos of the joint and site constraints when requesting a configuration. Ask the supplier to verify working range, mounting approach, power requirements and any accessories needed for the stated job. Keep this selection decision separate from the repair procedure: machining sequence and bore restoration methods depend on the damage and repair specification.
Questions buyers often ask
Can one boring machine cover excavators, loaders and cranes?
Possibly, if its working range, bar length, mounting options and accessories suit the different joints. Verify each target bore and setup rather than assuming one configuration fits every machine.
What information is needed for an on-site recommendation?
Provide bore diameter and length, spacing between bores, joint photos, access restrictions, available power and whether the equipment can be moved or dismantled.
Does a larger machine always suit heavier equipment?
No. The useful choice is the configuration that reaches and mounts securely at the bore while meeting the job’s dimensional and alignment requirements. Oversizing alone does not solve access or setup problems.
More Articles
-
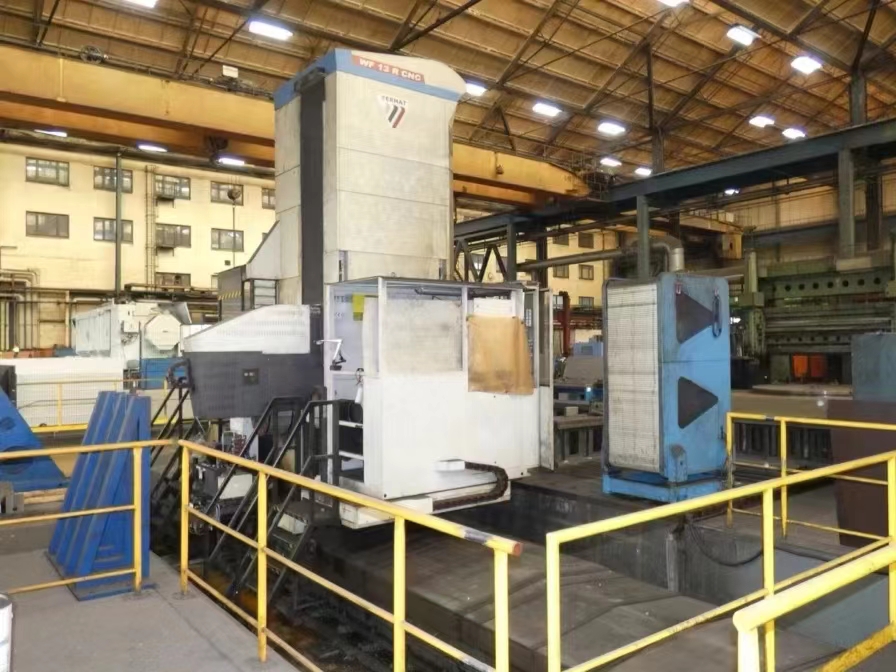
Portable vs Stationary Boring Machine: Key Differences for Industrial UseChoosing between a portable boring machine and a stationary boring machine depends on where the work must be performed, how the workpiece is supported, and how much setup the job can accept. Portable equipment is designed to bring line boring capability to large or immobile components. Stationary equipment is better suited to a controlled workshop environment with repeatable loading, alignment and production procedures. The right choice is therefore determined by the repair or machining situation, rather than by a universal winner. Two Different Industrial Use Cases A portable boring machine is generally selected when transporting the component is impractical. Typical situations include excavator booms, loader arms, crane structures, construction equipment frames and large machinery that must remain at a plant or worksite. The machine is positioned and secured around the damaged bore, allowing machining to take place in position. A stationary boring machine is installed in a workshop or production area. The component is brought to the machine, supported on the bed or fixture, and processed under controlled operating conditions. This arrangement is useful for repeat repairs, batch work, larger machining programs and components that can be safely moved. Portable vs Stationary Boring Machine: Direct Comparison Factor Portable boring machine Stationary boring machine Mobility Moves to the component; suitable for field or in-situ repair Remains in a fixed workshop location Installation Requires local setup, mounting, alignment and site preparation Uses established foundations, fixtures and workshop services Workpiece size Practical for oversized or non-transportable structures Limited by machine capacity, bed dimensions and handling equipment Operating environment May be exposed to restricted access, contamination or weather Offers a more controlled machining environment Best-fit work On-site repair, emergency restoration and large equipment Repeatable workshop repair, production and planned machining Trade-Offs That Affect the Decision Portability reduces transportation and disassembly requirements, but it shifts more responsibility to the jobsite. The team must verify access, mounting surfaces, structural stability, power availability, chip control and measurement access before machining begins. Setup quality directly affects alignment and final bore condition. Stationary equipment usually simplifies fixturing and process control. However, transporting a heavy component may require lifting equipment, permits, disassembly and additional downtime. The machine may also be unsuitable if the component exceeds its working envelope or cannot be positioned securely. For a repair involving one large machine that cannot leave service easily, the cost of mobilization and setup for portable equipment may be justified. For repeated components or planned workshop work, fixed fixturing and established procedures may improve consistency and throughput. Questions to Confirm Before Selecting Can the component be removed and transported without excessive downtime or handling risk? What are the required bore diameter, center distance, access limitations and alignment references? Does the worksite provide stable mounting points, power, lighting, lifting support and adequate chip management? Is the job a one-time field repair, or will similar components be machined repeatedly? FAQ Is a portable boring machine suitable for workshop work?Yes. It can be used in a workshop when the component is too large for a fixed machine or when in-position machining avoids disassembly. The workshop must still provide suitable support, alignment access and safe operating space. Which option is better for oversized equipment?A portable boring machine is usually the practical option when the equipment cannot be transported or exceeds the stationary machine's working envelope. The mounting and alignment plan should be confirmed before mobilization. Does stationary equipment always provide better results?Not automatically. A stationary machine benefits from controlled fixturing and workshop conditions, while a properly installed portable machine can solve alignment and repair problems directly on the equipment. The result depends on machine suitability, setup and process control.
-
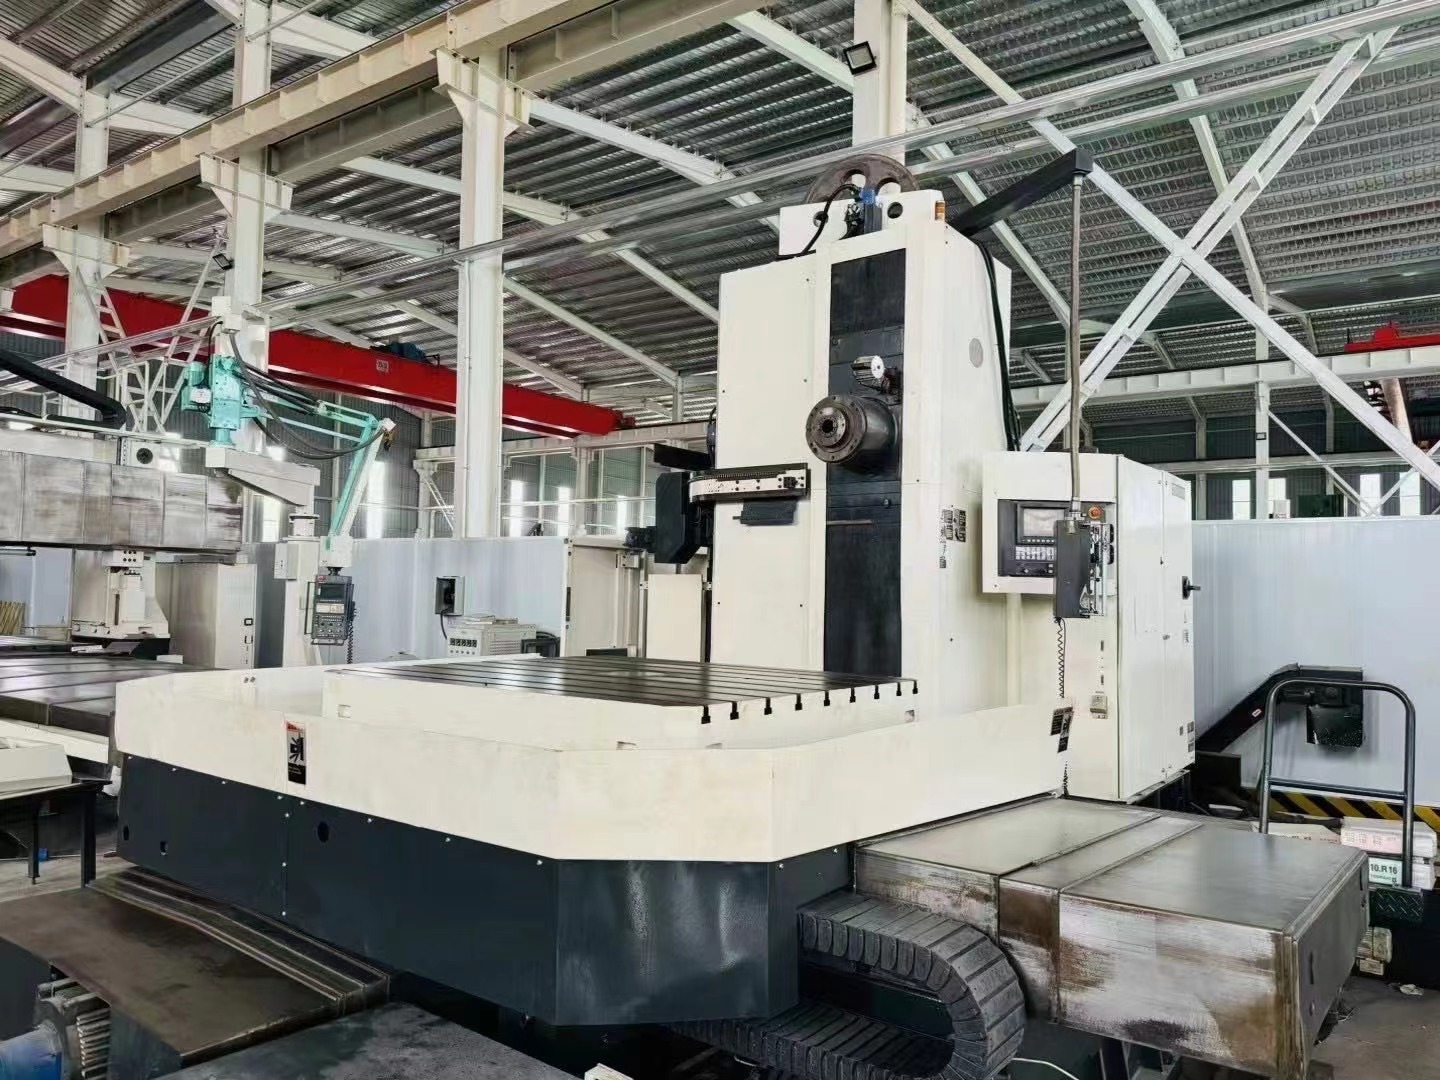
CNC Boring Machine Guide: Accuracy, Productivity and Application ConsiderationsFor repeat production of precision bores, a CNC boring machine should be evaluated against the part, batch size and required process sequence—not simply its control system. CNC motion and programmed cycles can improve consistency across repeated operations, but achieved accuracy also depends on machine condition, workholding, tooling, setup and measurement. Start with the production requirement Define the bore sizes and locations, workpiece material, number of operations, batch frequency and acceptance criteria. Include the full part envelope and the way parts will be loaded and clamped. These details determine whether the machine’s travel, spindle arrangement, workholding and tooling access suit the job. Ask suppliers to explain how they will demonstrate CNC boring machine accuracy on representative parts. Specify the measurement method, inspection locations and whether results should be checked after a warm-up or across repeated setups. A machine’s stated positioning performance is not, by itself, proof of finished-part accuracy. CNC control and repeatability The CNC system coordinates axis movement, spindle operation and programmed machining sequences. For recurring batches, saved programs reduce reliance on manual repositioning and make operation sequences easier to reproduce. Repeatability still depends on a stable datum, consistent clamping, tool condition, offset management and operator procedure. During evaluation, review the control functions the job actually needs: program storage and transfer, tool and offset management, cycle recovery, probing or measurement integration, and compatibility with the buyer’s programming workflow. Confirm who develops and validates the initial program, how revisions are controlled, and what operator training is included in the project scope. Productivity, automation and application fit Estimate cycle time from the complete sequence, including loading, clamping, tool changes, inspection and changeovers. Automation is worthwhile when it reduces a recurring constraint, such as frequent loading or unattended operation; its value depends on part variation, batch size, material flow and the need for in-process checks. Include integration, guarding, maintenance and recovery from interruptions in the assessment. Production scenario Assessment priority Configuration question Repeated parts in stable batches Program and setup repeatability Can proven workholding and tool offsets be reused? High-mix, low-volume work Changeover and programming effort How quickly can programs, tooling and fixtures change? Long cycles or frequent loading Utilization and operator time Would probing, automatic loading or monitoring address a real bottleneck? Large or complex workpieces Access, support and datum strategy Can the part be clamped and machined through the required sequence? Questions to resolve before specification How should accuracy be verified? Agree on a representative part test, inspection method and acceptance criteria before purchase. Does CNC automatically mean unattended production? No. Unattended running requires suitable part presentation, tool-life planning, monitoring, safety provisions and a defined response to faults. What should an automation quotation include? Clarify interfaces, fixtures, loading equipment, guarding, controls integration, commissioning responsibilities and operator training. Compare proposals using the same part, process sequence and production assumptions. This keeps CNC configuration, automation scope and expected output tied to measurable application needs.
-
Line Boring Machine: How It Works and Where It Is UsedWhen pivot bores, bearing housings or aligned holes become worn or misaligned, replacing the entire structure is often unnecessary. A line boring machine restores the bore axis and machining surface directly on the component, usually with the equipment positioned at the repair site. This makes line boring useful for heavy machinery where dismantling and transport would create excessive downtime. What Line Boring Corrects Line boring repairs a series of holes that must share one accurate centerline. Typical problems include enlarged bores caused by load and wear, oval holes, damage from loose bushings, and misalignment between opposing supports. The process is different from general boring because the cutting tool travels along a supported boring bar that references the existing structure. The objective is not simply to enlarge one hole, but to restore the relationship between multiple bores. How the Line Boring Process Works The repair begins with an inspection of the component, bore condition and access restrictions. A technician then mounts the boring bar supports and drive unit securely around the workpiece. Alignment is established from the required centerline, existing bore geometry or the repair drawing. Once the bar is stable and correctly positioned, the cutter removes material progressively along the bore. Finishing may include a final machining pass and preparation for a replacement bushing or bearing. The repaired geometry is then inspected before reassembly. Stage Purpose Typical decision Inspection Assess wear, damage, access and reference points Confirm whether on-site line boring is suitable Setup Install supports, boring bar and drive system Choose stable mounting positions and cutter access Alignment Establish the required common bore axis Set the repair datum and verify bar position Boring Remove damaged material in controlled passes Select a sequence that protects rigidity and surface quality Finishing Complete the final bore surface and fit condition Prepare for bushing, bearing or pin installation Inspection Verify the finished bore and alignment Record measurements before equipment assembly Line Boring Machine Applications Common line boring machine applications include excavator boom and arm pivots, loader and crane joints, bulldozer frames, agricultural equipment, mining machinery, marine structures and industrial equipment with aligned bearing seats. The method is especially valuable where the component is too large to move economically or where removing it would interrupt production. Restoring the original centerline can also support accurate bushing installation and reduce uneven loading during operation. Why Buyers Specify On-Site Line Boring On-site line boring can reduce dismantling, heavy transport and machine downtime, but the result depends on access, structural rigidity, alignment references and the condition of surrounding material. Buyers should provide photographs, bore dimensions, component drawings if available, equipment model, site restrictions and the required repair outcome when requesting a field repair assessment. These details allow the service provider to confirm tooling suitability, measurement requirements and the practical scope of work. FAQ Can line boring correct two misaligned bores? Yes. When the component can be securely supported, the boring bar can establish a common axis and machine the related bores in line. The required reference and material condition must be assessed before work begins. Is line boring only used on heavy equipment? No. Heavy equipment is a major use case, but the process also applies to industrial, marine, agricultural and structural components with aligned bores that require restoration. What information is needed for a line boring quotation? Useful information includes bore locations and dimensions, photographs, equipment type, access conditions, material or bushing details, site location and any available drawings or measurement records.
-
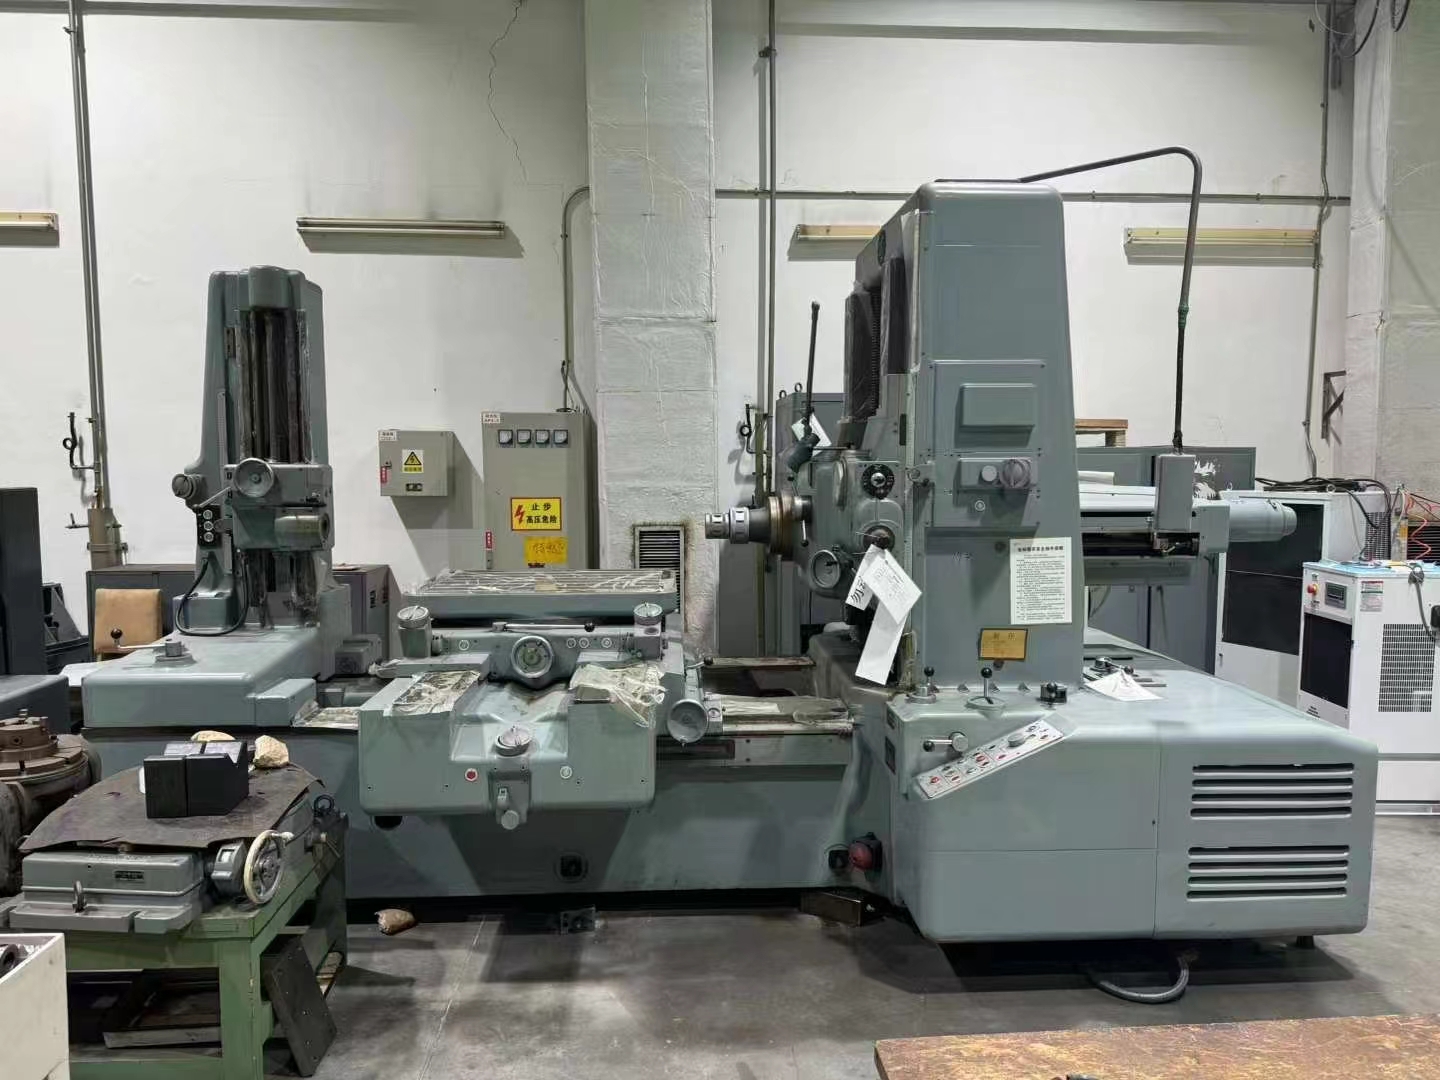
Horizontal Boring Machine: Applications, Key Features and Selection GuideWhen a workpiece is too large, heavy or structurally complex for a conventional machining center, a horizontal boring machine can provide the working envelope, spindle reach and rigidity required for accurate internal machining. Its horizontal spindle arrangement is suited to large castings, fabricated structures, gear housings and machinery bases that must be bored, drilled, milled or inspected in a controlled setup. The correct selection depends on more than nominal machine size. Buyers should match the machine to the workpiece envelope, required bore diameter, part weight, spindle travel, table or floor mounting arrangement, material and accuracy requirements. Why the Horizontal Configuration Matters In a horizontal boring machine, the spindle approaches the workpiece along a horizontal axis. This layout supports large components that are difficult to orient vertically and allows several related operations to be completed without repeatedly repositioning the part. For heavy workpieces, support from a rigid table, foundation or fixture helps control vibration and cutting deflection. The result is more predictable bore geometry, especially when machining deep holes, aligned bearing seats or multiple bores that must share a common centerline. Actual performance still depends on machine condition, tooling, fixturing, cutting parameters and operator practice. Key Selection Criteria for Large Workpieces Selection factor What to verify Why it affects the decision Workpiece envelope Maximum length, width, height and required access around the part Determines whether the component can be loaded, positioned and machined without interference Workpiece weight Table, foundation, fixture and loading-system capacity Insufficient support can increase vibration, deflection and setup risk Bore requirements Diameter range, bore depth, spindle travel and tool reach Defines whether the machine can complete the hole in one stable setup Accuracy and rigidity Required alignment, surface finish and repeatability, plus machine condition Heavy-duty boring demands structural stability throughout the cutting cycle Process scope Need for milling, drilling, tapping, facing or multiple setups Broader capability may reduce handling and secondary operations Horizontal Boring Machine Applications Common horizontal boring machine applications include machining hydraulic-cylinder housings, engine and transmission cases, pump bodies, gearbox housings, machine bases, construction-equipment components, shipbuilding parts and large welded fabrications. The machine is especially suitable when bore alignment, perpendicularity and positional accuracy matter across a large component. Fixed horizontal equipment is generally selected for planned production or heavy repair work in a machining facility, where the part can be transported to the machine and securely fixtured. Portable line boring equipment serves a different situation: it is used when the component is difficult to move and machining must be performed at the installation site. The decision should therefore begin with logistics and setup location, not only bore diameter. Questions Buyers Should Confirm Is a horizontal boring machine suitable for every large workpiece?Not necessarily. The part must fit the machine envelope, loading method and fixture arrangement, and its weight must be compatible with the supporting structure. Does a larger machine automatically provide better accuracy?No. Accuracy depends on rigidity, alignment, thermal condition, spindle and feed condition, tooling, fixturing and verification methods as well as nominal size. When should portable equipment be considered instead?Consider portable line boring when moving the damaged or installed component is impractical. Choose fixed horizontal equipment when controlled shop-floor setup, broader machining capability and repeatable workholding are the priority.