CNC Boring Machine Guide: Accuracy, Productivity and Application Considerations
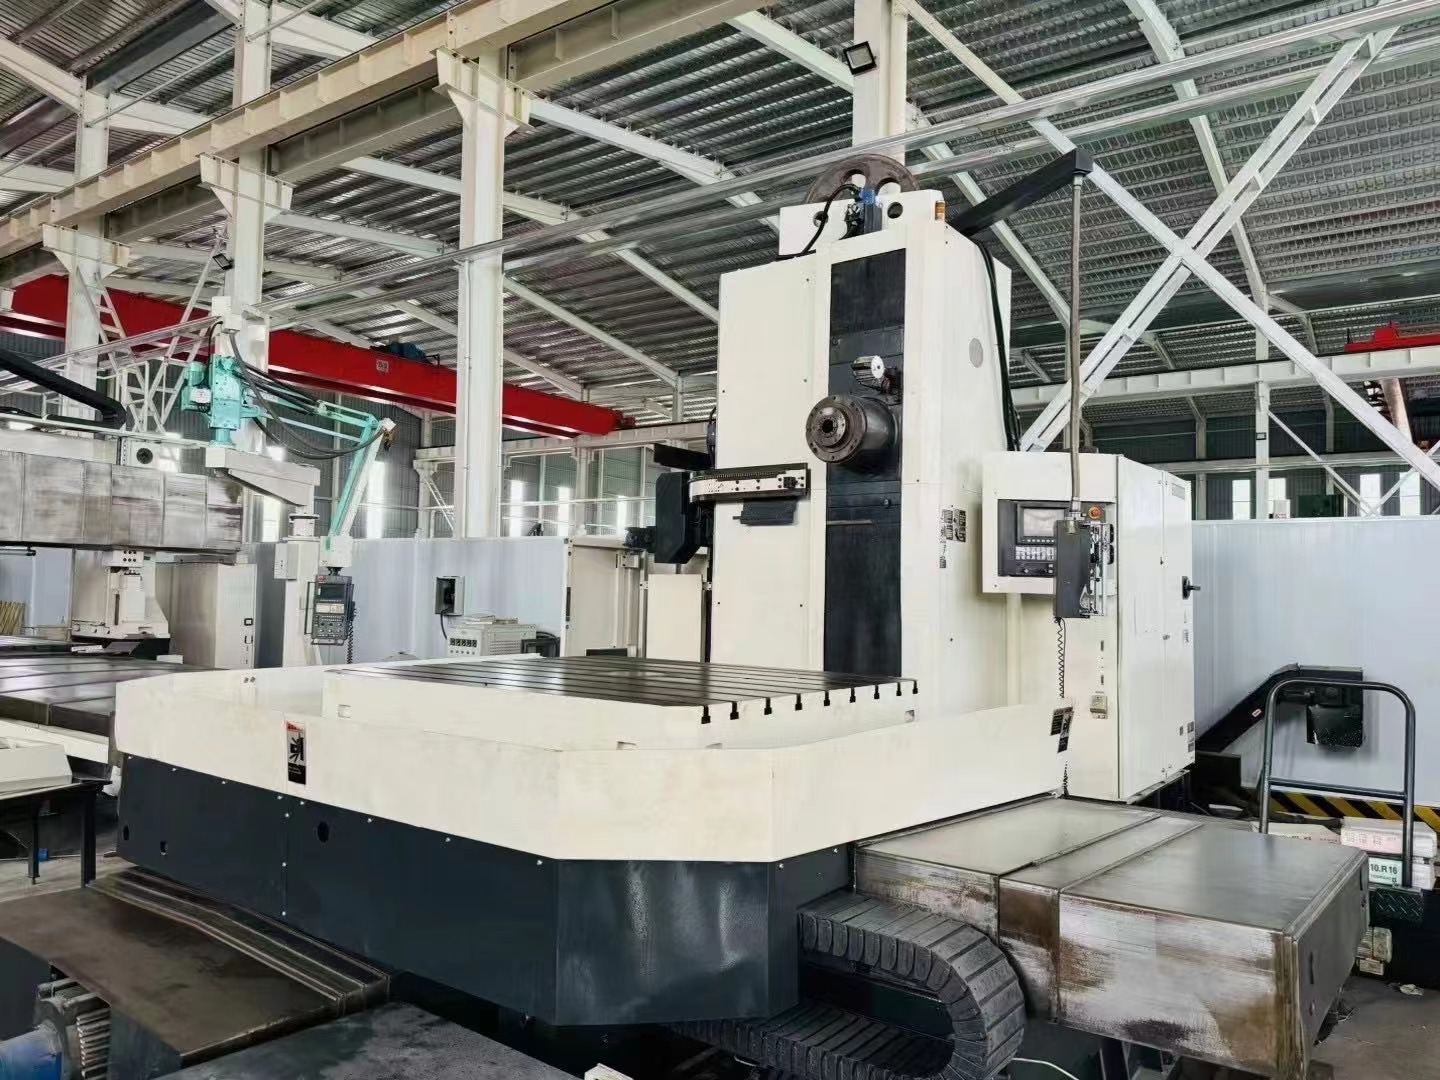
For repeat production of precision bores, a CNC boring machine should be evaluated against the part, batch size and required process sequence—not simply its control system. CNC motion and programmed cycles can improve consistency across repeated operations, but achieved accuracy also depends on machine condition, workholding, tooling, setup and measurement.
Start with the production requirement
Define the bore sizes and locations, workpiece material, number of operations, batch frequency and acceptance criteria. Include the full part envelope and the way parts will be loaded and clamped. These details determine whether the machine’s travel, spindle arrangement, workholding and tooling access suit the job.
Ask suppliers to explain how they will demonstrate CNC boring machine accuracy on representative parts. Specify the measurement method, inspection locations and whether results should be checked after a warm-up or across repeated setups. A machine’s stated positioning performance is not, by itself, proof of finished-part accuracy.
CNC control and repeatability
The CNC system coordinates axis movement, spindle operation and programmed machining sequences. For recurring batches, saved programs reduce reliance on manual repositioning and make operation sequences easier to reproduce. Repeatability still depends on a stable datum, consistent clamping, tool condition, offset management and operator procedure.
During evaluation, review the control functions the job actually needs: program storage and transfer, tool and offset management, cycle recovery, probing or measurement integration, and compatibility with the buyer’s programming workflow. Confirm who develops and validates the initial program, how revisions are controlled, and what operator training is included in the project scope.
Productivity, automation and application fit
Estimate cycle time from the complete sequence, including loading, clamping, tool changes, inspection and changeovers. Automation is worthwhile when it reduces a recurring constraint, such as frequent loading or unattended operation; its value depends on part variation, batch size, material flow and the need for in-process checks. Include integration, guarding, maintenance and recovery from interruptions in the assessment.
| Production scenario | Assessment priority | Configuration question |
|---|---|---|
| Repeated parts in stable batches | Program and setup repeatability | Can proven workholding and tool offsets be reused? |
| High-mix, low-volume work | Changeover and programming effort | How quickly can programs, tooling and fixtures change? |
| Long cycles or frequent loading | Utilization and operator time | Would probing, automatic loading or monitoring address a real bottleneck? |
| Large or complex workpieces | Access, support and datum strategy | Can the part be clamped and machined through the required sequence? |
Questions to resolve before specification
- How should accuracy be verified? Agree on a representative part test, inspection method and acceptance criteria before purchase.
- Does CNC automatically mean unattended production? No. Unattended running requires suitable part presentation, tool-life planning, monitoring, safety provisions and a defined response to faults.
- What should an automation quotation include? Clarify interfaces, fixtures, loading equipment, guarding, controls integration, commissioning responsibilities and operator training.
Compare proposals using the same part, process sequence and production assumptions. This keeps CNC configuration, automation scope and expected output tied to measurable application needs.
More Articles
-
Custom Boring Machine Solutions for OEM ProjectsA custom boring machine becomes necessary when standard equipment cannot meet the bore geometry, mounting access, cutting load or site conditions of a repair or production job. Before commissioning a new design, establish whether approved tooling, supports or drive options can resolve the limitation. That distinction determines the engineering scope and prototype requirements. Translate equipment limitations into engineering requirements Specify the finished bore and the installation constraints together. A machine may cover the required diameter yet lack clearance for its drive, sufficient bar support or a practical mounting position on the workpiece. Custom requirement Engineering response to evaluate Nonstandard bore diameter or deep reach Bar diameter, support spacing, cutting head geometry and usable travel Irregular workpiece or restricted access Dedicated fixtures, bearing mounts and drive placement Special material or interrupted cuts Toolholder rigidity, insert selection, speed range and torque Site power or environmental constraints Drive compatibility, controls, cooling and protection appropriate to exposure Prepare a brief that supports design review For a custom line boring machine, provide drawings showing bore locations, diameters, spacing, datum references and machining allowances. Add material details, hardness where known, dimensional and geometric tolerances, surface finish requirements, and photographs showing surrounding obstructions. Include available electrical or hydraulic supply, operating orientation, ambient conditions, duty cycle and handling limits. Ask the supplier to identify assumptions, exclusions and which requirements need a cutting trial. Confirm its actual OEM/ODM scope: branding or packaging services alone do not establish machine design capability. Approve the prototype before releasing production Agree on acceptance criteria before fabrication. Engineering review should address bar deflection, fixture rigidity, tool access, chip removal and safe setup. Prototype trials should use representative material and geometry, with results recorded against the agreed bore dimensions, alignment and surface finish. For an OEM boring machine program, approve drawings, the bill of materials, control configuration and inspection records before batch release. Define checks for purchased components, assembly and final function, plus how design changes are authorized. Confirm branding artwork, manuals, spare parts identification and packaging for the intended transport and storage conditions. Establish first-article approval and repeat-unit inspection requirements in the purchase agreement. Custom project FAQ What does the customization process involve? Requirements review, feasibility assessment, design approval, prototype manufacture, acceptance testing and controlled production. Confirm deliverables and approval responsibilities at each stage. Can a project start without complete drawings? An initial review can use sketches, measurements and photographs. Final design approval needs verified dimensions, datums and acceptance criteria; complex access constraints may require a site survey or 3D model. How should prototype quality be confirmed? Require a documented inspection and cutting trial under agreed conditions. Record instruments, measurement methods and results, and close any deviations before approving production.
-
Boring Machine Setup Guide: Key Steps for Accurate On-Site MachiningA reliable boring machine setup begins before the first cut. On-site machining accuracy depends on the condition of the damaged bore, the rigidity of the installation, correct boring bar alignment and measurements taken at each critical stage. Always follow the equipment manufacturer’s manual, approved safety procedures and the specific requirements of the repair project. 1. Inspect the Work Area and Damaged Bore Confirm that the machine, support points, workpiece and surrounding area are suitable for on-site machining. Remove loose debris, oil contamination and obstructions that could affect mounting or measurement. Inspect the existing bore for cracks, distortion, weld buildup, broken fasteners or damage that may change the machining plan. Check access for the boring bar, drive unit, power supply and measuring tools. Identify lifting, guarding and lockout requirements before installation. If the workpiece is unstable or access is restricted, correct those conditions before continuing rather than compensating through cutting adjustments. 2. Measure Before Alignment Record the existing bore condition and the relationship between the bore, surrounding faces and available support locations. Use suitable calibrated measuring equipment and take readings at more than one position where access permits. These measurements establish the starting condition and help determine whether the proposed boring bar travel and final machining allowance are adequate. Do not assume that a visually clean bore is straight or concentric. Taper, ovality, offset and wear can affect alignment decisions. Document the readings so the final result can be compared with the project requirement. 3. Align and Secure the Boring System Boring bar alignment should be established from the required finished bore location, not simply from the edge of the existing hole. Position the support bearings or mounting brackets according to the machine manual and the workpiece geometry. Check the bar position at multiple reference points, then adjust until the axis matches the required machining centerline. After alignment, tighten all mounting hardware in the specified sequence and verify that the supports remain stable. Secure the workpiece and machine against movement, vibration and accidental contact. Recheck alignment after tightening because clamping force or uneven support can shift the boring bar. 4. Set Cutting Parameters and Bore Set tool projection, feed, rotational speed and depth of cut according to the machine manual, tool condition, material, bore size and required finish. Use conservative starting conditions when the material condition or rigidity is uncertain. Confirm tool clearance, rotation direction, chip evacuation and guarding before starting the drive. During the cut, monitor vibration, unusual noise, tool wear and mounting movement. Stop the operation if the setup changes or if cutting conditions become unstable. A controlled setup is more important than forcing a higher removal rate. 5. Verify the Finished Bore After machining, clean the bore and measure the finished diameter at the locations required by the project specification. Check for taper, ovality, surface damage and the required relationship to adjacent features. Record the final results and compare them with the acceptance criteria before removing the equipment. Frequently Asked Questions How long does an on-site boring machine setup take? There is no universal installation time. The duration depends on access, bore size, mounting complexity, alignment requirements, site conditions and the inspection process. Confirm the expected schedule from the equipment manual and project plan rather than using a fixed estimate. How is the boring bar aligned? Measure the required bore axis, position the supports and adjust the bar at multiple reference points. Recheck alignment after all supports and clamps are tightened. Which setup errors affect accuracy most? Unstable supports, incorrect centerline measurement, bar deflection, workpiece movement and failure to recheck alignment can directly affect bore size, straightness and concentricity. What must be checked before machining starts? Verify mounting security, bar clearance, tool condition, power and controls, guarding, workpiece stability, measurement records and the approved cutting parameters.
-
Boring Machine Accuracy: Key Factors That Affect Machining ResultsA bore can meet its diameter requirement yet still fail assembly because its axis is misplaced, its shape is distorted or adjacent bores are misaligned. Boring machine accuracy therefore needs to be assessed against the drawing’s dimensional, geometric and surface finish requirements. For portable line boring repairs on excavator pivots, loader frames and similar assemblies, the machine, mounting arrangement and workpiece form one machining system. Published machine capability alone cannot establish the finished result. Accuracy Factors Checklist Factor Effect on results Control before finishing Machine and bar rigidity Deflection and vibration can produce taper, chatter or size variation. Minimize unsupported bar length and tool overhang; check supports and bearing condition. Alignment and mounting An incorrect bar axis produces bores in the wrong position. Reference approved datums and recheck alignment after securing mounts. Tool condition and cutting parameters Wear, built-up edge and excessive cutting forces alter size and finish. Check insert condition, tool clamping, speed, feed and depth of cut. Workpiece condition Clamping distortion, weld stress and heat can change geometry. Inspect cracks, weld repairs, support points and temperature. Measurement method Limited sampling or unsuitable gauges can miss defects. Use calibrated instruments with resolution and uncertainty appropriate to the tolerance. Control the Setup Before Adjusting the Cut Establish the required bore axis from the drawing or an approved repair reference. Worn bores may no longer represent the original centerline. For line boring accuracy, verify the relationship between all relevant bores, rather than centering independently on each damaged opening. Secure the component and supports, then check that the bar rotates freely and the alignment remains stable. Stop the drive before adjusting tools or supports. A light trial cut can reveal chatter or uneven engagement, but it does not prove positional accuracy. Select cutting parameters for the material, insert and setup rigidity. Excessive cutting force can deflect the bar; an excessively light cut can cause rubbing. Leave controlled finishing stock, monitor tool wear and investigate dimensional drift before continuing. Verify Size, Form and Axis Separately Clean and deburr the bore before inspection. Measure diameter at multiple depths and angular positions to screen for taper and ovality. These readings alone do not establish roundness, cylindricity or coaxiality; use an inspection method suited to each drawing requirement. Account for workpiece and instrument temperature. Where clamping may distort the component, agree whether acceptance measurements apply in the clamped or released condition. Record the setup, measurement locations and results. Accuracy and Alignment FAQ Does correct alignment guarantee an accurate bore? No. Alignment establishes the intended axis, while rigidity, tooling, cutting conditions and workpiece stability determine whether machining maintains it. What information is needed to assess achievable accuracy? Provide bore dimensions, spacing, material, required tolerances, datum references, repair history, access restrictions and the proposed inspection method. Any accuracy commitment should be confirmed for those conditions.
-
How to Choose a Boring Machine for Excavator and Loader RepairsChoosing a boring machine for excavator repair starts with the damaged part. Pin bores, bucket linkages and boom connections place different demands on alignment, access and machine setup. For loader work, the same principle applies to articulation points and pivot bores. Identify the repair location first, then match the machine to the bore diameter, available working space and required installation method. Match the machine to the damaged component Equipment Part Typical Repair Requirement Excavator pin bores Restore worn or oval bores while keeping the bore aligned through the connected lug structure. Bucket linkage Repair multiple linkage bores with controlled positioning around compact, obstructed assemblies. Boom and arm connections Handle larger pivot bores and maintain alignment between separated mounting ears. Loader articulation points Recondition central hinge and pin bores where access, clearance and machine positioning affect setup. Loader pivot bores Remove wear and prepare the bore for a replacement or repaired pin with consistent geometry. Start with the bore problem Excavator pin bores commonly develop ovality, uneven wear and clearance around the pin. A suitable boring machine for excavator repair should allow the operator to establish a stable reference, align the cutting bar with the original bore centerline and remove only the material needed for the repair. If several connected bores are involved, the machine must support a setup that preserves their relationship. For bucket linkage and boom or arm connections, access can determine machine fit. Check whether the boring bar can pass through the assembly, whether the mounting points provide enough room for supports, and whether nearby hydraulic lines or structural members restrict positioning. A compact setup may be essential for on-site repair, while a larger and more rigid arrangement may suit a major pivot bore. Requirements for a boring machine for loader repair Loader articulation points and pivot bores require careful attention to alignment because the repaired bore affects hinge movement and pin loading. Before selecting equipment, record the bore diameter, bore length, distance between bores, access direction and available clearance around the loader frame. These details help determine the cutting-bar arrangement, support placement and whether the repair can be completed without removing the full assembly. Site conditions also influence the choice. Confirm the power supply, lifting and handling options, working height, weather exposure and space for measurement and machining. Buyers should verify the machine’s usable diameter range, boring-bar length, mounting method, alignment procedure and suitability for the specific excavator or loader component. Information to send before requesting a recommendation Equipment type and the exact repair location Measured bore diameter, length and wear condition Pin dimensions and whether bushes will be installed Photos showing access, obstructions and surrounding structure On-site or workshop repair conditions, including available power This information allows a supplier to assess machine fit against the actual repair rather than the equipment model alone. FAQ: excavator and loader bore repairs Can one machine repair excavator pin bores and loader articulation points? It may, if its diameter range, bar length, support arrangement and mounting options suit both components. Verify each repair dimension and access condition before selecting a general-purpose setup. What should be measured on a worn excavator bore? Measure the existing bore diameter at several positions, identify ovality and taper, record bore length, and check the mating pin and surrounding lug alignment. These measurements define the machining allowance and setup requirements. What information is needed for a boring machine for loader repair? Provide the loader model, articulation or pivot location, bore and pin dimensions, photos of the working area, access direction, clearance and site power conditions.