Premium Used & Refurbished Machine Tools | High Precision Industrial Machinery
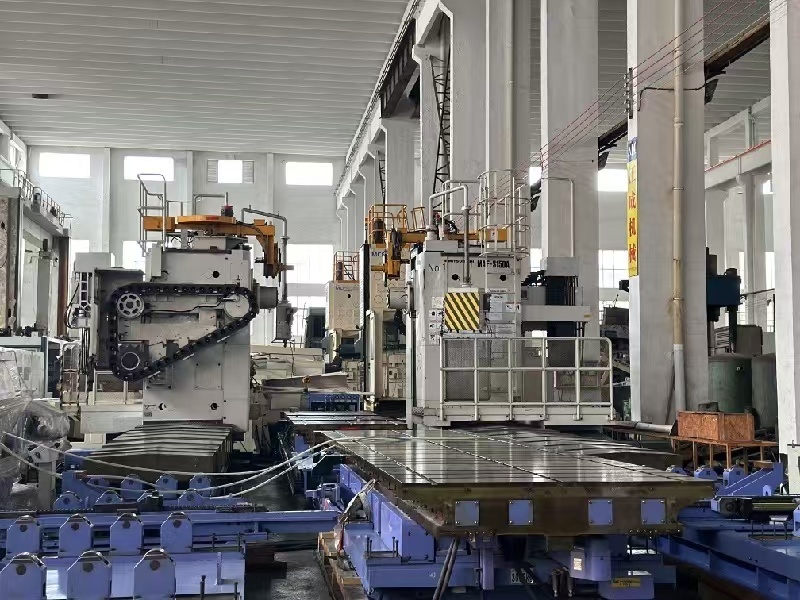
Manufacturing enterprises worldwide pursue stable machining quality and low equipment investment. Brand-new machine tools bring high costs and long delivery cycles, restricting factory capacity expansion. We are a professional supplier focusing on high-quality used machine tool sales and standard refurbishment services. We provide reliable, high-precision reconditioned machinery for global metalworking factories, helping businesses reduce procurement costs while maintaining stable production efficiency.
1. Advantages of Used & Refurbished Machine Tools
Refurbished industrial machinery is the best cost-effective solution for modern manufacturing. Compared with new equipment, qualified refurbished machine tools save up to 50% of procurement funds, effectively reducing the financial pressure on small and medium-sized factories.
Moreover, our refurbished machines support fast delivery. Unlike new machines with long production cycles, our inspected and reconditioned equipment is in stock and can be delivered quickly, allowing factories to start production in the shortest time. With professional refurbishment processing, these machines eliminate common problems such as low precision and unstable operation of ordinary second-hand equipment, reaching near-new industrial working standards.
2. Our Complete Machine Tool Product Range
We supply a full series of mainstream industrial machine tools for global customers. Our product line covers CNC machining centers, CNC lathes, milling machines, grinders, drilling machines and boring machines, covering all needs of mold processing, hardware manufacturing and mechanical parts production.
All equipment is strictly screened from formal industrial manufacturers. We eliminate faulty, modified and aging machines with poor performance. Each machine undergoes strict structural inspection, electrical testing and running detection before refurbishment to ensure basic mechanical stability and processing performance, providing reliable raw equipment for subsequent precision renovation.
3. Standard Professional Refurbishment Process
We adopt standardized international refurbishment procedures to guarantee machine tool quality. First, our engineers fully disassemble the machine to inspect core components such as spindles, guide rails, bearings and screw rods. All worn and aging parts are replaced with high-quality standard accessories.
Next, we optimize and debug the entire electrical, hydraulic and pneumatic systems to eliminate hidden operational faults. After assembly, we conduct high-precision calibration of positioning accuracy and flatness. Every machine passes 72-hour continuous load testing to ensure stable operation. Finally, we complete rust removal and professional painting to restore a brand-new appearance for industrial workshop use.
4. Core Strengths of Our Services
Our refurbished machine tools own obvious market advantages. First, stable high precision. All reconditioned equipment meets industrial precision standards, fully adapting to mass production and high-precision processing work. Second, low failure rate. Updated core parts and optimized systems greatly reduce later maintenance costs.
Third, we support customized refurbishment and function upgrading according to customer production demands. Whether you need precision improvement or system update, we can provide tailored solutions. Ultra-high cost performance and long service life make our equipment ideal for factory expansion, new workshop investment and cost-controlled production projects.
5. Reliable One-Stop After-Sales Support
We provide full-process services including equipment selection, technical consultation, export packaging and global logistics. Overseas customers can enjoy complete export documents and safe door-to-door delivery solutions.
We offer official warranty and lifelong remote technical support. During the warranty period, all non-human damage faults are solved with free maintenance and part replacement. Adhering to transparent pricing and strict quality control, we have won trust from global manufacturing clients. Contact us now to get free quotations and professional machine tool solutions for your factory.
More Articles
-
What to Consider When Buying a Boring Machine from a ManufacturerA boring machine manufacturer should be evaluated against your repair or production task—not simply its catalog range. Before requesting a quotation, provide workpiece drawings, bore dimensions, material, access restrictions, required geometry and finish, and expected duty cycle. For portable line boring, include mounting locations and site power. These details let you assess whether the supplier can engineer a workable solution rather than merely quote a machine. Check who controls engineering and production Ask which activities the supplier performs directly: design, machining, assembly, control integration and final testing. Outsourcing is not automatically a weakness; unclear responsibility is. A credible industrial boring machine supplier should identify who controls critical components, supplier qualification and corrective action. Request a live factory walkthrough or an independent audit covering machines comparable to your proposed configuration. General workshop footage does not establish application competence. Ask an engineer to explain the proposed setup, tooling reach, support arrangement and limitations. Manufacturer Evaluation Checklist Area Evidence to request Risk to resolve Engineering Application review and proposed configuration Unverified assumptions about access, rigidity or tooling Production control Process responsibilities and critical-component records Uncontrolled substitutions or unclear accountability Quality control Inspection plan, calibration records and sample reports Claims unsupported by measurement Machine testing Agreed cutting test and acceptance report No-load demonstration mistaken for machining proof Lifecycle support Parts list, warranty terms and service procedure Downtime without a clear recovery route Make acceptance measurable before ordering Agree on factory acceptance testing before paying a deposit. Define the test material, tooling, setup, cutting conditions, measurements and pass/fail criteria. A spindle-running video cannot demonstrate bore accuracy or surface finish under load. For a boring machine factory, quality evidence should connect component inspection, assembly checks and final testing to the delivered machine. Specify who witnesses testing, which records accompany shipment, and how failures are corrected and retested. Where site conditions affect results, distinguish factory acceptance from commissioning checks. Verify customization and post-delivery responsibility For custom configurations or OEM/ODM projects, document design ownership, branding, drawing approval, software access and change control. Confirm whether modifications affect parts availability or service documentation. Request written warranty coverage, exclusions, claim procedures and responsibility for labor, travel and freight. Verify spare-part identification, quoted availability, remote troubleshooting and commissioning arrangements. For exports, clarify packing, shipping documents, destination compliance responsibilities and manuals; export capability alone does not establish suitability for your country. Supplier audit and procurement FAQ Is a factory visit essential? Not always. A live remote audit, independent inspection and witnessed cutting test can reduce risk. Higher-value or heavily customized projects justify deeper verification. How should competing manufacturers be compared? Issue the same application brief and acceptance requirements. Compare documented technical fit, exclusions and support obligations—not headline price or claimed factory size.
-
Boring Machine Maintenance Guide: How to Keep Equipment Running ReliablyReliable boring machine maintenance starts with controlling contamination, friction, cutting forces and alignment errors before they become downtime. A practical maintenance program should follow the machine’s operating conditions and manufacturer instructions rather than rely on one fixed service interval. Before inspection or cleaning, isolate power and secure moving components according to the applicable safety procedure. Cleanliness and lubrication protect moving components Chips, abrasive dust and coolant residue can enter slideways, bearings, gearboxes and electrical enclosures. This contamination increases friction and can cause sticking, accelerated wear or overheating. Remove chips with suitable tools, wipe exposed surfaces, and keep slideways, feed screws, spindle areas and clamping surfaces free from debris. Do not direct high pressure air toward bearings, seals or control cabinets. Check lubrication points, oil levels and grease condition against the machine manual. Confirm that lubricant reaches the intended bearing, slideway or gear. Excess lubricant can attract abrasive material, while insufficient lubricant increases temperature and wear. Inspect for leaks and identify the source before simply adding more lubricant. Inspect tools, boring bars and alignment A damaged insert or dull cutter increases cutting force and may produce vibration, poor surface finish and oversize bores. Check inserts, holders and tool clamping before each job. Replace damaged cutting edges and verify that the tool is seated securely. Record recurring edge damage because it may indicate excessive load, poor chip evacuation or incorrect cutting conditions. The boring bar is especially sensitive to deflection, runout and unsupported length. Inspect the bar for scoring, bending, damaged threads and worn mounting surfaces. Clean the bar, holder and spindle interface before assembly. If the machine shows taper, chatter or inconsistent bore size, check tool runout, workpiece clamping and machine alignment before changing cutting parameters. Check the drive, motor and electrical system Abnormal noise, heat, vibration, odor or unstable speed can indicate problems in the motor, drive, bearings or power connections. Keep cooling paths clear and inspect accessible cables, connectors, switches and protective devices for damage or looseness. Electrical enclosure filters and fans should remain clean so heat can escape. When an alarm, repeated trip or irregular motion occurs, stop the machine and record the operating condition, alarm code and recent maintenance work. Qualified personnel should test electrical components and determine whether the cause is mechanical resistance, a control fault or a power issue. Maintenance checklist and spare parts planning Maintenance Item Recommended Check Cleaning Remove chips, dust and coolant residue from slides, tooling, guards and work areas. Lubrication Verify lubricant level, delivery and leakage using the machine manual. Tooling and boring bar Check inserts, runout, mounting surfaces, deflection and clamping security. Motor and electrical system Inspect cooling, cables, connectors, alarms, vibration and abnormal temperature. Storage Clean, dry and protect exposed machined surfaces; release or secure components as specified. For long-term storage, clean and dry the machine, apply the specified corrosion protection, cover it in a dry ventilated area and follow the manufacturer’s instructions for batteries, lubricants and movable axes. Keep commonly replaced inserts, seals, filters, fuses and other model-specific items identified by part number. Confirm compatibility before ordering; the correct spare part depends on the machine version and assembly. FAQ How often should a boring machine be maintained? Use operating hours, load, environment, coolant exposure and manufacturer guidance to set inspection intervals. Cleaning and visual checks may be needed more frequently in abrasive or high-chip environments. What should be checked when bore accuracy changes? Inspect the tool edge, boring bar runout, clamping, spindle condition, lubrication and machine alignment. Check one factor at a time and document the result. Which spare parts should be kept available? Identify wear items and failure-prone components from the machine manual and service history. Verify part numbers, revisions and interchangeability with the equipment supplier before purchase.
-
Boring Machine Bore Diameter: How to Choose the Right Machining RangeChoosing the correct boring machine bore diameter starts with the workpiece, not the machine catalogue. The finished bore, existing hole condition, access length and material determine whether a machine can complete the job efficiently. A quoted maximum diameter alone does not show whether the machine can enter the smallest hole or maintain a practical setup across the full machining range. Start with the workpiece and the finished bore Record the smallest and largest bore diameters that the machine must produce. Also note whether the hole is a through bore, blind bore, stepped bore or aligned set of holes. Measure the available access around the workpiece and the distance from the mounting position to the bore centerline. The minimum bore diameter must allow the boring bar, cutting tool and any required support components to enter the hole with safe clearance. The maximum bore diameter must include the actual cutting diameter required after considering the existing hole, machining allowance and finishing pass. If a job involves several bore sizes, use the complete range rather than selecting the machine from the largest size only. Use the real boring machine working range Workpiece condition Range to verify Why it matters Small existing hole Minimum tool and bar entry diameter Determines whether the tool can reach the bore without interference. Large repair bore Maximum finished cutting diameter Confirms that the machine can remove the required material and finish the bore. Deep or offset bore Boring bar length and support position Controls reach, clearance and the usable portion of the diameter range. Stepped or multiple bores Complete diameter sequence Shows whether one configuration can cover the job without repeated changes. The usable boring machine working range is narrower than a headline range when the workpiece requires a long reach, large material removal or restricted access. Confirm the machine's operating diameter at the required boring bar length, because a configuration suitable for a short bore may not provide the same practical capability at greater depth. Match boring bar length, tooling and material Boring bar length should be based on the distance from the mounting point to the deepest cutting location. Select the shortest bar that reaches the required position while preserving clearance. Excessive length can reduce rigidity and limit practical cutting conditions, especially in hard steel or interrupted repair surfaces. Tool selection also affects the usable bore range. Small diameters may require compact cutters and suitable insert clearance; larger diameters may require a different bar, cutter arrangement or support method. Cast iron, carbon steel, alloy steel and other materials can require different cutting tools and machining approaches. These choices should be confirmed together with the diameter and reach rather than treated as separate specifications. Submit actual dimensions for configuration confirmation Before ordering, provide the supplier with the smallest and largest finished bore, existing bore sizes, bore depth, workpiece material, machining allowance, access restrictions and required bore locations. A drawing or clear dimensional sketch allows the supplier to confirm the machine range, boring bar length and tooling configuration for the actual repair or production task. FAQ Is the maximum bore diameter enough for machine selection? No. The minimum bore, required reach, cutting allowance and tool clearance are equally important. A machine may reach the largest diameter while being unsuitable for the smallest hole or deepest section. How does boring bar length affect the machining range? A longer bar extends reach but can change the practical working range because access, rigidity and tool clearance become more restrictive. Confirm the diameter range at the required reach. What information should be sent for a bore range check? Send the real workpiece drawing or dimensions, finished bore range, existing hole sizes, bore depth, material, allowance and access conditions. These details support configuration confirmation before purchase.
-
Boring Machine Applications in Construction Equipment RepairWhen a pin joint develops play, replacing the pin alone may not solve the problem. Wear can leave the housing bore oval, tapered or out of alignment. A boring machine for construction equipment repair restores the bore so the joint can be fitted with a correctly sized pin or bush. This work is often performed on the machine in the field when removing a large component would add substantial downtime. Where bore wear occurs on construction equipment Repeated articulation, impact loading, inadequate lubrication and contamination can wear the bores that support pins and bushes. The repair target is the damaged joint bore, not simply the visible pin. Before machining, the technician needs to identify the joint layout, access, material condition and the relationship between connected bores. Equipment Typical bore Repair purpose Excavator Boom, arm and bucket pin bores Restore pin fit and joint alignment Loader Lift-arm and bucket pivot bores Correct wear at heavily cycled pivots Backhoe Dipstick, boom and stabilizer pin bores Re-establish fit across linkage joints Crane Boom and linkage pivot bores Address wear at structural articulation points Hydraulic equipment Cylinder-end and mounting pin bores Restore the connection between cylinder and structure How boring repair addresses the damage Construction equipment boring repair typically starts with inspection and measurement. The repair team checks bore diameter, roundness, wear pattern and alignment with related bores. If the housing is suitable for repair, a portable line boring setup machines the damaged bore to a controlled, consistent diameter. Depending on the repair plan, the bore may then receive a bush, or be finished to suit the specified pin or bearing arrangement. Where two or more bores form one pivot line, their alignment matters as much as the individual diameters. Machining them in a common setup can help restore the intended axis. The required dimensions and fit should come from the equipment specification or an agreed repair drawing; they should not be assumed from the pin size alone. Field conditions shape the repair plan Access, nearby structures, available setup space and the condition of the surrounding material affect whether on-site boring is practical. Cracks, severe distortion, damaged welds or a bore near a highly loaded structural area may require additional inspection or a different repair sequence. The machine must also be isolated and securely supported before work begins, following site and equipment safety procedures. For a field assessment, document the machine and joint location, report the symptoms, and provide measurements or photographs where available. Confirm whether connected bores need to be machined on the same axis, whether a bush will be installed, and what final fit is required. These details help establish a realistic repair scope before equipment is mobilized. Frequently asked questions Which excavator parts commonly need bore repair? Boom, arm and bucket pin joints are common locations, as are other pivot connections showing looseness or uneven wear. Inspection determines whether the bore, pin, bush or several parts need attention. Can loader pivot bores be repaired on site? Often, but feasibility depends on access, setup conditions, damage severity and the required machining sequence. A site assessment can establish whether portable boring is appropriate. Does every worn bore need a new bush? No. The repair method depends on the equipment design, bore condition and specified fit. Confirm the intended finished dimensions and component arrangement before machining.